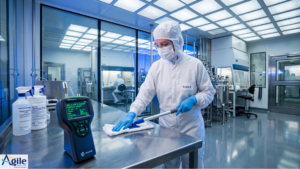
A single airborne particle or chemical residue can ruin a production batch, compromise research validity, or trigger an FDA warning letter. Maintaining controlled environments demands precise execution, certified chemistry, and continuous verification. Managing sanitation across varied ISO classifications requires balancing stringent micro-cleanliness in critical zones with operational efficiency in surrounding buffer areas.
Developing standardized cleanroom cleaning protocols across ISO Class 5 through ISO Class 9 environments establishes verifiable, audit-ready compliance for cGMP facilities, biotech plants, and advanced data facilities.
Understanding ISO 14644-1 Cleanroom Classifications and Micro-Contaminant Risks
Cleanroom sanitation standards are governed by ISO 14644-1, which defines air cleanliness by airborne particle concentration.
ISO Class 5 vs. ISO Class 9 Particle Threshold Standards
Cleanroom requirements vary drastically based on classification thresholds:
| ISO Class | Max Particles (≥0.5μm/m3) | Standard Environment Type | Primary Cleaning Focus | Minimum Cleaning Frequency |
| ISO Class 5 | 3,520 | Aseptic Filling, Semiconductor Bay | Ultra-low particulate removal, bioburden eradication | Daily / Shift Change |
| ISO Class 6 | 35,200 | Pharmaceutical Preparation | Micro-particle control, non-linting wipe-downs | Daily |
| ISO Class 7 | 352,000 | Secondary Packaging, Medical Device Assembly | Surface residue elimination, HEPA-assisted vacuuming | Daily to Bi-Weekly |
| ISO Class 8 | 3,520,000 | Staging Areas, Gowning Rooms | Gross contamination control, floor scrub protocols | Weekly / Semi-Weekly |
| ISO Class 9 | 35,200,000 | Ambient Buffer Zones, Air Locks | Particulate containment, entry barrier maintenance | Weekly / As Needed |
ISO Class 5 environments permit no more than 3,520 particles () per cubic meter, demanding daily specialized decontamination. In contrast, ISO Class 9 represents an ambient baseline permitting up to 35,200,000 particles per cubic meter, serving primarily as a buffer zone to prevent particulate migration into cleaner spaces.
Common Sources of Contamination in High-Tech & Life Science Facilities
- Human Shedding: According to the National Environmental Balancing Bureau (NEBB), personnel generate over 70% of cleanroom contamination through skin flakes, hair, and clothing fibers.
- Material Transfer: Raw materials and equipment moving into controlled zones introduce exterior dust, packaging debris, and cross-contaminants.
- Outgassing and Chemical Residues: Off-gassing solvents, aggressive non-neutral cleaners, and improper sealants alter room chemistry and leave microscopic residues on contact surfaces.
- HVAC Deficiencies: Turbulent airflow or degraded HEPA filtration allowed particulate settling on critical work surfaces.
Standard Operating Procedures (SOPs) for Controlled Environment Sanitation
Maintaining ISO controlled environment cleaning standards requires disciplined SOP execution that prevents cross-contamination across boundaries.
[Personnel Entry & Gowning] ➔ [Top-Down HEPA Vacuuming] ➔ [Controlled Surface Wiping] ➔ [Chemical Disinfection] ➔ [Quantitative Verification]
Proper Gowning, Personnel Entry, and Material Transfer Protocols
Preventing cross-contamination starts at the threshold. Staff and third-party specialists must follow strict entry protocols before stepping into sensitive zones:
- Step-Off Pad and Sticky Mat Maintenance: Place adhesive mats at all transition zones. Peel top sheets daily or when visual saturation reaches 50%.
- Top-Down Gowning Sequence: Don protective wear from head to toe (hood, mask, coverall, booties, double gloves) to ensure shed particles fall onto ungarbed surfaces during the process.
- Material Pass-Through Sanitation: Spray and wipe all incoming equipment, containers, and tools with sterile 70/30 Isopropyl Alcohol (IPA) inside the airlock before introducing them to the cleanroom floor.
HEPA Vacuuming, Particle Control, and Microfiber Surface Sanitation
Physical cleaning must capture and remove contaminants rather than redistributing them.
- ULPA/HEPA Vacuuming: Use sealed, exhaust-filtered vacuums rated at 99.999% efficiency at to pull particulates from walls, coving, and flooring joints.
- Continuous-Filament Microfiber: Deploy ultra-low particulate, laser-cut polyester or continuous-filament microfiber mops. Never use woven cotton or standard commercial mop heads that shed fibers.
- Unidirectional Squeegee and Wiping Technique: Wipe surfaces in straight, overlapping parallel strokes away from HEPA supply vents toward return air ducts. Never wipe in circular motions, which re-deposits particles across clean zones.
Chemically Compatible, Non-Off-Gassing, pH-Balanced Cleaning Chemistry
Chemical selection must eliminate bioburden without damaging expensive stainless steel, polycarbonate, or epoxy flooring.
- Rotational Disinfectant Strategy: Alternate between broad-spectrum quaternary ammonium compounds and sporicidal agents (such as peracetic acid/hydrogen peroxide blends) to prevent microbial resistance.
- Zero Off-Gassing Requirements: Utilize high-purity, low-VOC chemistries designed specifically for cGMP facility cleaning. Avoid cleaners containing silicates, phosphates, or heavy perfumes.
- pH Balance and Material Compatibility: Use non-corrosive neutral cleaners (pH 6.0-8.0) on sensitive equipment housings to prevent pitting, micro-cracking, and subsequent bacterial harborage
Generating Audit-Ready Documentation and Service Tracking
Regulatory agencies like the FDA do not simply inspect physical cleanliness; they inspect proof of process. If an action is unrecorded, regulatory frameworks treat it as unperformed.
Time-Stamped Service Logs and Task Execution Checklists
Audit readiness depends on full transparency and chain-of-custody documentation:
- Digital Task Logs: Service technicians complete digital logs recording precise entry/exit times, chemical lot numbers, expiration dates, and specific task executions.
- SOP Deviations: Any variance from standard protocol (e.g., chemical contact time adjustments, equipment malfunctions) must trigger an immediate exception log and root-cause analysis note.
Utilizing ATP Swab Testing and Particle Counters for Standardized Verification
Quantitative testing validates that cleaning procedures achieve specified standards.
- ATP Swab Testing Facility Protocols: Adenosine Triphosphate (ATP) bioluminescence testing detects biological residue on high-touch surfaces. Swab results under 10 RLU (Relative Light Units) confirm effective organic removal prior to disinfection.
- Particle Count Testing Cleanroom Metrics: Perform airborne particle measurements using calibrated optical counters immediately following cleaning cycles (at-rest validation) to verify compliance with ISO 14644-1 limits.
Mitigating Product Loss and Regulatory Risk with Certified Cleaning Specialists
Outsourcing cleanroom maintenance to non-specialized janitorial providers exposes facilities to severe operational risks, including batch rejections, unscheduled downtime, and regulatory fines. Specialized cleanroom cleaning partners bring:
- Trained Personnel: Technicians certified in ISO/cGMP protocols who understand cleanroom physics, air balance, and contamination control.
- Validated Tooling: Dedicated, color-coded, non-shedding tools and dedicated cleanroom-grade HEPA equipment that remain strictly within designated clean zones.
- Turnkey Audit Readiness: Standardized reporting platforms that generate immediate verification data for regulatory reviews.
Protect your high-value production environment from contamination risks. Contact Agile Facility Solutions today to discuss our controlled environment cleaning services and secure audit-ready compliance for your facility.